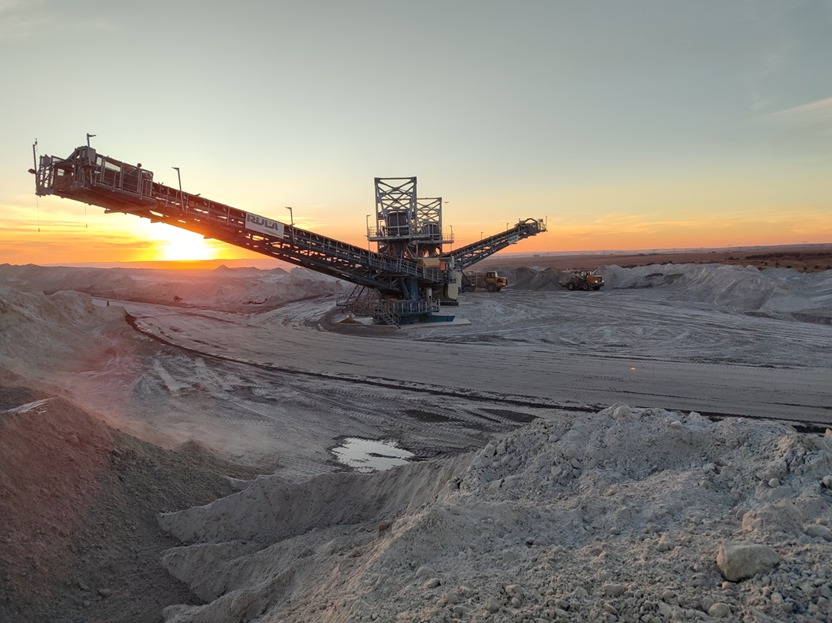
Radial stackers are essential for stockyard management, enabling organized storage of coal, ore, aggregates, and other bulk materials. With slewing booms, adjustable heights, and automated controls, they maximize stockpile capacity while integrating with conveyors for seamless flow across industrial facilities.
Applications
Stockyard stacking for mining, quarrying, and port operations
Handling coal, aggregates, ores, and biomass
Large-scale stockpile formation and inventory management
Integration with upstream conveyors and silos
Benefits
Efficient use of yard space with radial stacking
Automated slewing and boom elevation control
Environmental compliance with dust suppression options
High-capacity discharge tailored to materials and belts
RULA Expertise
Engineering stackers for 20–50 m boom lengths
Designing slewing and elevating systems (hydraulic/electric)
Integrating PLC automation for material flow control
Safety integration: limit switches, guardrails, and monitoring