Bucket elevators provide efficient vertical transportation of fine and coarse bulk materials to silos and elevated process areas through controlled loading and discharge. The enclosed design promotes a cleaner operating environment, while optimised bucket geometry and operating speeds ensure reliable material handling, reduced carry-back, and improved product integrity.


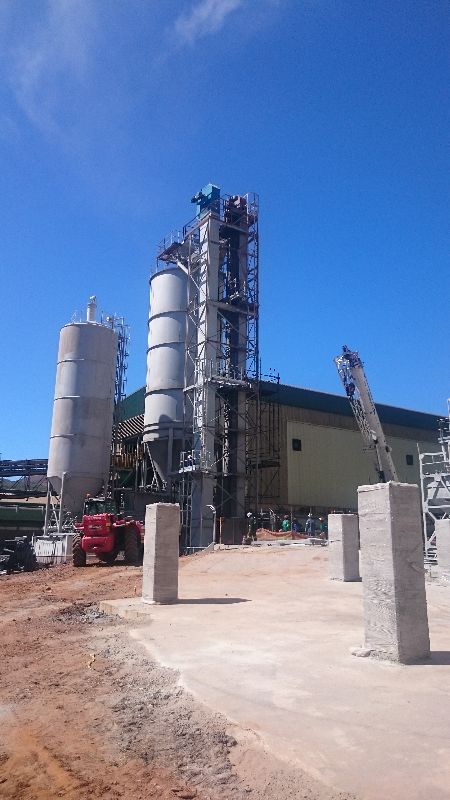
Material enters via a precision-engineered inlet chute at the elevator boot, designed to optimize feed dynamics.
Bucket geometry, head housing, and discharge chutes are tailored to operational speeds, ensuring effective discharge with minimal spillage.
Designs are validated using Discrete Element Method (DEM) simulations for comprehensive material flow and wear analysis.
Crowned head and tail pulleys maintain belt alignment, while wear-resistant bucket edges and adjustable throat plates mitigate re-entrainment.
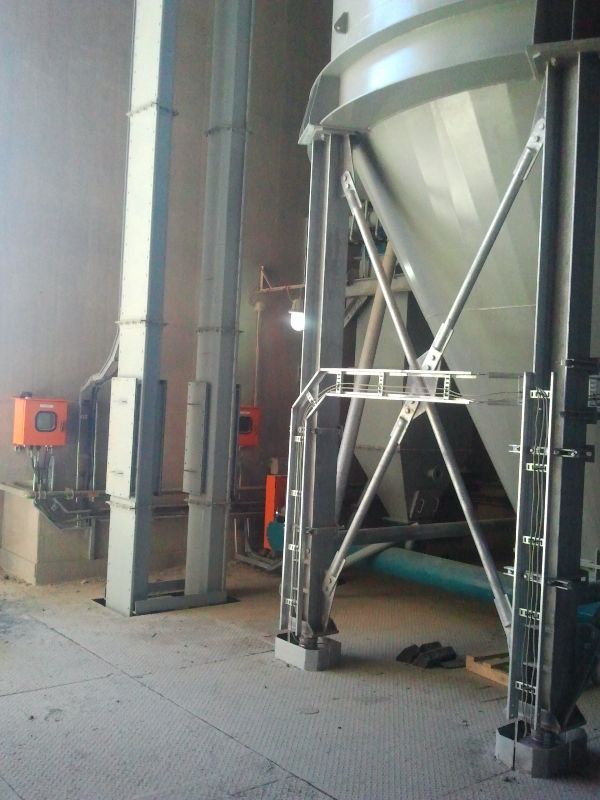
Our systems feature advanced monitoring, including misalignment switches, boot level switches, and tail pulley speed sensors to enhance operational control.
Optional features such as access platforms, support brackets, hoist frames, cat ladders, rotation sensors, and belt drift detectors provide flexibility across diverse plant requirements.
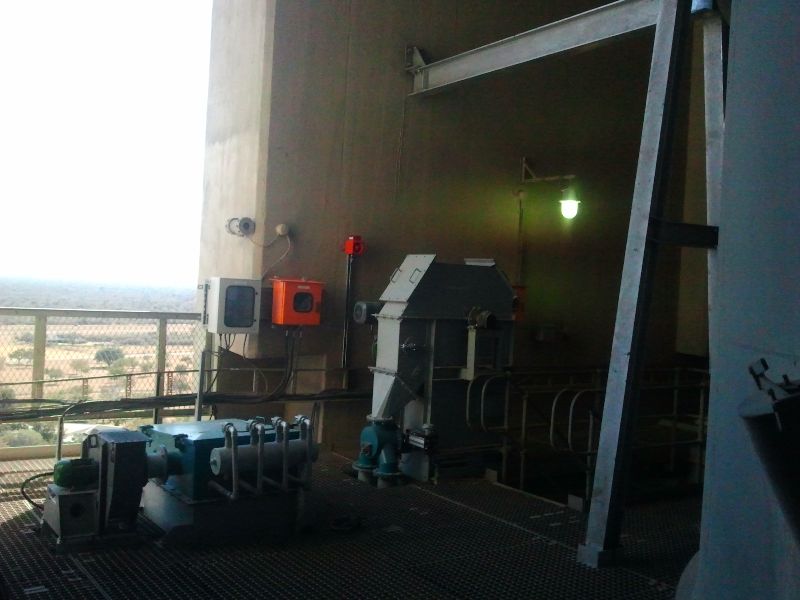
RULA's vertical transport solutions are engineered for high-availability across any industrial footprint.