RULA Bulk Materials Handling Tube Chain Conveyors provide a dust-free and spill-resistant solution, specifically engineered for the reliable transportation of powders, granules, and heavy aggregates.
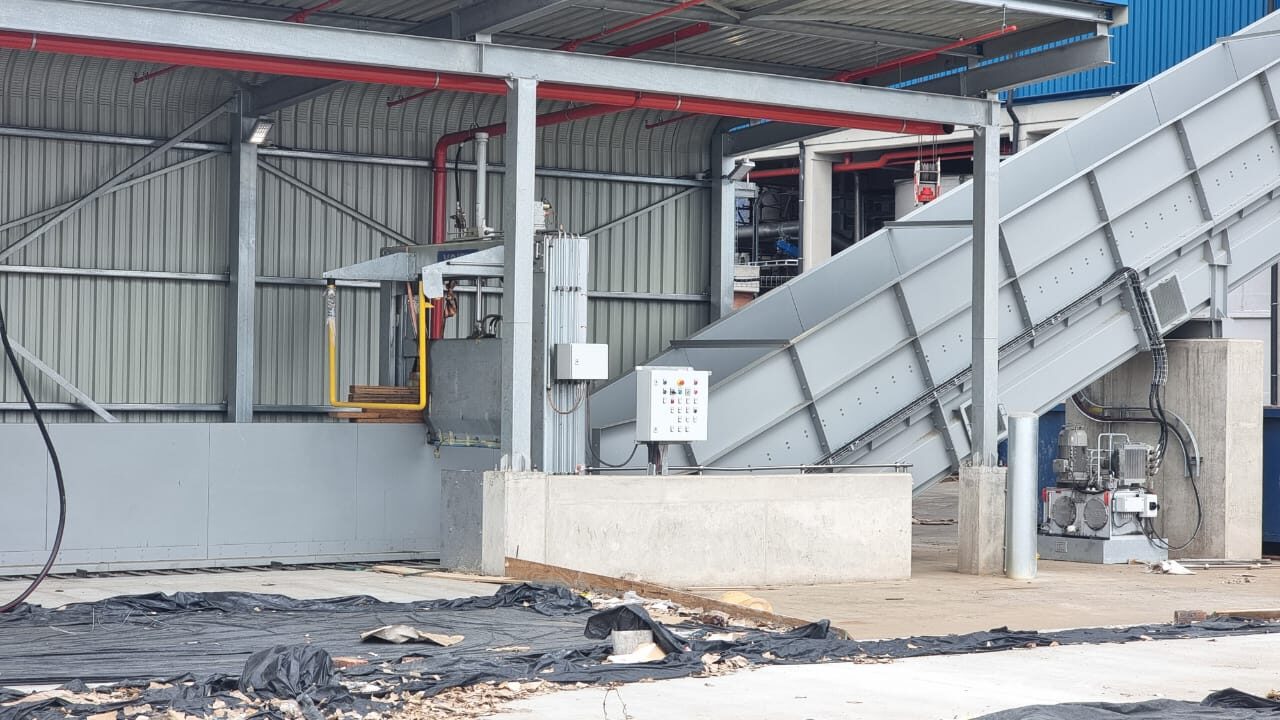
A robust chain enclosed within a tubular casing ensures material containment and reliable flow, effectively minimizing dust, spillage, and contamination.
Operates seamlessly in horizontal, vertical, or inclined configurations, adapting to the dynamic spatial demands of modern industrial operations.
Engineered for the rigorous demands of mining and cement industries, capable of handling heavy and highly abrasive materials with high availability.
The motor-driven chain system is designed for high energy efficiency and low maintenance requirements, ensuring a cost-effective operational lifecycle.
Bulk materials are loaded at the conveyor intake, where the motor-driven chain moves the material along the tube. Specialized chain flights scoop and transport the material, discharging it at the end point into the receiving system.
The entire operation is supported by end stations that allow for smooth transition, while advanced seals and lubrication systems ensure long-lasting, efficient performance in sensitive applications.